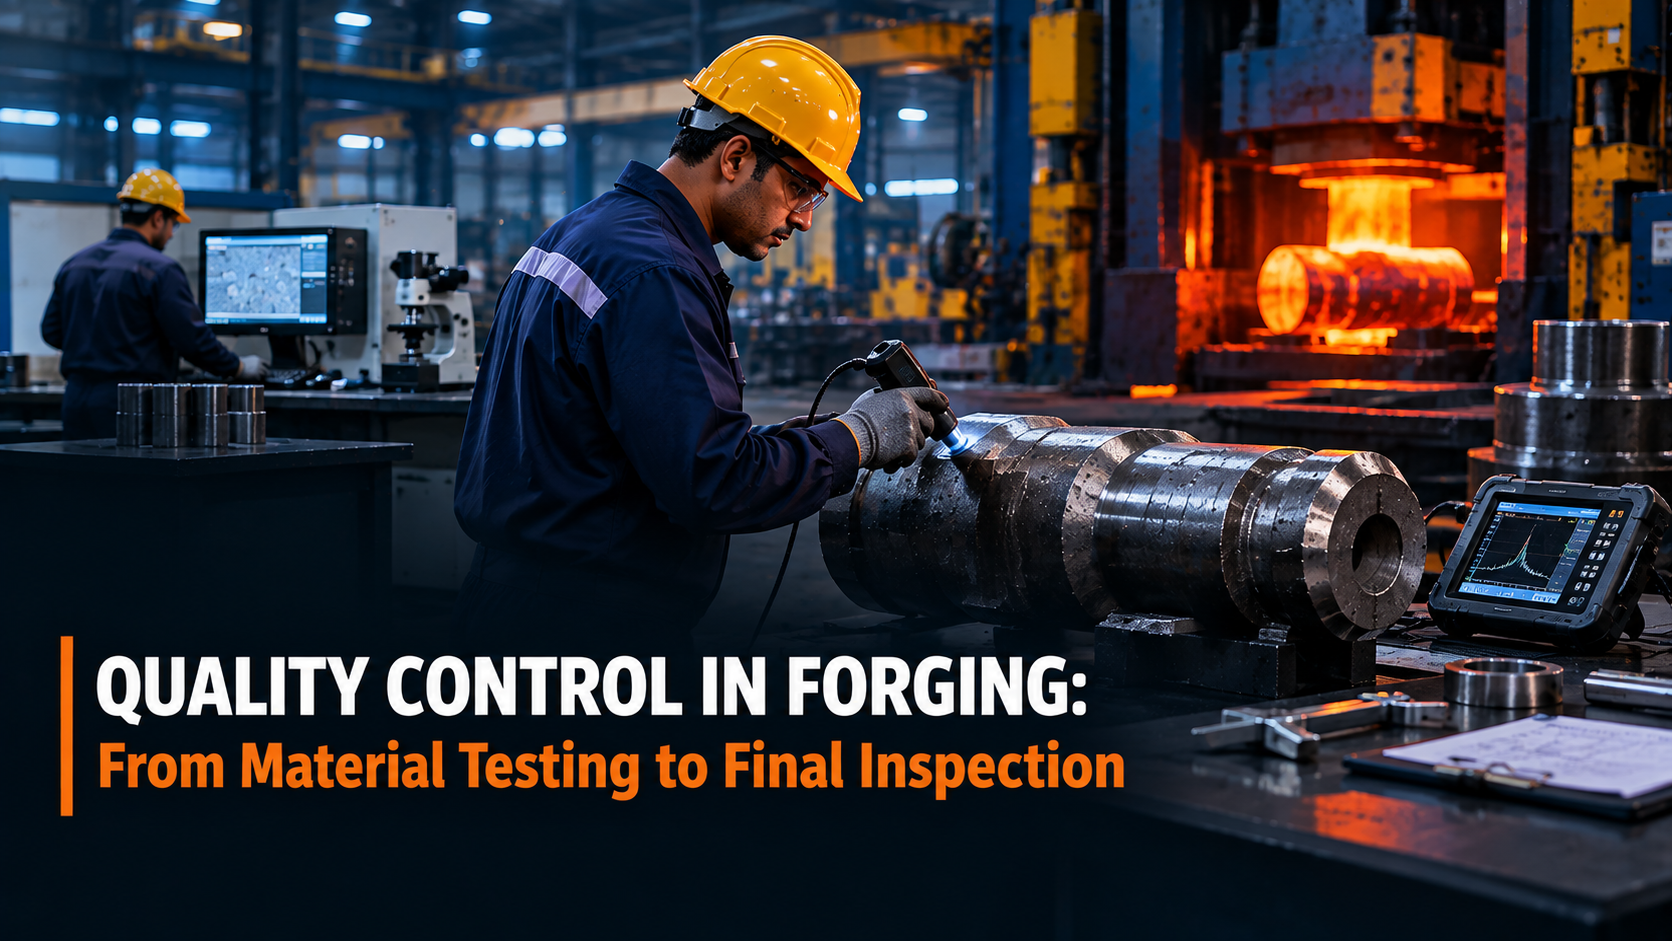
Some defects cannot be identified through visual inspection alone. This is where Non-Destructive Examination (NDE) becomes important.
Forged industrial components—such as heavy step shafts, proof-machined rings, gear blanks, and high-pressure blocks—are engineered for mission-critical machinery. In service, these parts endure severe cyclic vibrations, fluctuating thermal gradients, and massive mechanical stresses. While visual metrology verifies dimensional geometry, subsurface flaws like hydrogen flakes, thermal quench bursts, micro-inclusions, or tight forging laps remain completely invisible to the naked eye. Non-Destructive Examination (NDE) provides the specialized diagnostic techniques needed to inspect internal and surface soundess without altering or damaging the workpiece.
Ultrasonic Testing (UT)
Ultrasonic Testing, or UT, uses high-frequency sound waves to examine components and identify certain internal discontinuities.
UT represents the primary volumetric inspection methodology for heavy open die forgings. Because open die forgings can feature ruling cross-sections up to 800 mm in diameter, penetrating the entire cross-sectional thickness requires advanced pulse-echo acoustics:
How Ultrasonic Testing Works
A piezoelectric transducer converts electrical pulses into high-frequency acoustic waves (typically 1.0 MHz to 4.0 MHz). The probe travels along a proof-machined surface with an acoustic couplant (oil, cellulose gel, or water). Sound waves propagate through the sound steel matrix and reflect back from both the opposite boundary (back-wall echo) and any internal interfaces.
If an internal discontinuity—such as an ingot shrinkage cavity, non-metallic inclusion cluster, porosity, or hydrogen flake—lies in the sound beam’s path, a distinct intermediate echo is displayed on the flaw detector screen, pinpointing the flaw’s exact depth, amplitude, and coordinate.
- Straight Beam (Longitudinal Wave) Scanning: Performed perpendicularly to flat and cylindrical surfaces (bars, blocks, and blanks) to map general volumetric integrity and back-wall attenuation.
- Angle Beam (Shear Wave) Scanning: Deploys angled wedges (typically 45°, 60°, or 70°) to inspect complex fillets, stepped transition shoulders, inner bore radii, and radial discontinuities in forged rings.
- Governing Standards: Executed strictly according to ASTM A388, EN 10228-3, and ASME Section V standards by certified Level II NDE specialists.
Magnetic Particle Inspection (MPI)
MPI can be used to detect certain surface and near-surface discontinuities in suitable ferromagnetic materials.
While ultrasonic testing inspects the interior volume, Magnetic Particle Inspection (also termed Magnetic Particle Testing or MT) provides unmatched sensitivity for detecting tight surface and near-surface cracks in carbon and low-alloy ferromagnetic steels:
Magnetic Flux Leakage Principle
The forged component is magnetized using an AC/DC electromagnetic articulating yoke or direct contact prods. Magnetic flux lines travel unimpeded through sound ferromagnetic material. When a crack, seam, or forging lap crosses these flux lines, the flux leaks out into the surrounding air, creating magnetic north and south poles across the defect.
Finely divided iron oxide particles (suspended in oil or water carrier) applied to the surface are immediately drawn to the leakage field. Under white light (black ink) or ultraviolet UV-A black light (fluorescent suspension), this forms sharp, high-contrast indications that reveal fine micro-cracks that would otherwise escape visual detection.
- Primary Flaws Detected: Forging laps, flash line tears, cooling cracks, quench cracks, and machining/grinding checks.
- Governing Standards: Performed according to ASTM A275, ASTM E709, and EN 10228-1 specifications with verified magnetic field strength indicators (pie gauges / Gauss meters).
Liquid Penetrant / Dye Penetrant Testing (LP/DP)
LP/DP testing can help identify surface-breaking discontinuities.
Liquid Penetrant Examination (PT), commonly called Dye Penetrant Inspection (DPI), relies on capillary action to identify defects that break the outer surface of non-porous metals. It is particularly vital for materials where Magnetic Particle Testing cannot be utilized:
Capillary Action & Developer Bleed-Out
A low-viscosity penetrant with high surface wetting capability is applied across the thoroughly degreased component. Given adequate dwell time (10 to 30 minutes), the dye seeps deep into open microscopic surface fissures by capillary action.
Excess surface penetrant is wiped away, and a chalk-like developer is sprayed over the area. The developer acts as a blotter, reversing the capillary action and drawing trapped dye back up to the surface, creating vivid, magnified red indications against a bright white background.
- Non-Magnetic Material Solution: Indispensable for austenitic stainless steels (e.g., SS 304, SS 316), duplex stainless steels, and nickel-based superalloys where magnetic fields cannot be induced.
- Governing Standards: Executed in full compliance with ASTM E165 and EN 10228-2.
Comparative Overview of NDE Methods
Selecting the proper examination technique depends on the component's geometry, alloy composition, and whether internal volume or surface boundaries require scrutiny:
| NDE Method | Inspection Scope | Material Suitability | Key Discontinuities Found |
|---|---|---|---|
| Ultrasonic Testing (UT) | Full Volumetric (Core to Surface) | All fine-grained carbon, alloy, and stainless steels | Porosity, inclusions, shrinkage, hydrogen flakes, internal bursts |
| Magnetic Particle (MPI) | Surface & Shallow Subsurface (~2–3 mm) | Ferromagnetic materials only (carbon and alloy steels) | Forging laps, seams, quench cracks, fatigue fissures |
| Liquid Penetrant (LP/DP) | Surface-Breaking Flaws Only | Non-magnetic steels, stainless, nickel alloys, and non-ferrous metals | Surface cracks, cold shuts, pinholes, grinding cracks |
Why NDE Matters
NDE allows manufacturers to examine components without destroying or permanently damaging them. It can be particularly valuable for components where internal integrity is critical.
Traditional destructive evaluation—such as tensile sectioning, Charpy impact breaking, or deep macro-etching—provides valuable benchmark data but consumes the tested specimen. In contrast, NDE delivers definitive insights on the actual production parts that will be deployed into active service:
- Preserving 100% of Production: Components undergo thorough volumetric and surface inspection and proceed directly to assembly or dispatch with zero reduction in structural life.
- Preventing Catastrophic Field Failures: Unchecked internal flaws in turbine shafts, crane hooks, or heavy rings can lead to abrupt fatigue propagation under cyclic operation. NDE acts as a vital safety barrier.
- Early Stage Economics: Conducting proof-machining followed by early Ultrasonic Testing (UT) prevents spending expensive machine hours on finish CNC contouring of a billet containing central ingot piping or gross metallurgical flaws.
Forgewell Industries: Quality Assurance You Can Trust
Forgewell incorporates inspection and NDE capabilities into its manufacturing and quality processes according to applicable customer and component requirements.
At Forgewell Industries, all NDE procedures are performed and evaluated by certified ASNT / ISNT Level II inspectors working in strict accordance with ISO 9001:2015 quality frameworks and OEM drawings. Equipped with calibrated digital ultrasonic flaw detectors, standardized reference test blocks, electromagnetic yokes, and NABL-traceable metrology instruments, our inspection regime guarantees that every component meets rigorous international standards.
Quality built into the process. Confidence in the final component.